Nadcap certification is not a general quality-system approval. It is a process-specific assessment of whether an aerospace supplier can repeatedly perform a special process under controlled conditions, with evidence that the process produces conforming results. A company may hold a recognized quality-management certification and still be unprepared for Nadcap if its shop-floor controls, equipment records, personnel qualifications, or technical instructions do not meet the expectations for the process being audited.
For aerospace suppliers, the practical question is not simply “Can we pass an audit?” It is whether the documented process, the equipment condition, the operator’s actions, and the released product record all tell the same defensible story. This is especially important for heat treatment, chemical processing, coatings, non-destructive testing, welding, and other operations where defects may not be visible after manufacture but can affect fatigue life, strength, corrosion resistance, or flight safety.
Start with the scope, not the audit date
The first preparation decision is to define the exact Nadcap scope that applies to the work performed. A heat-treatment facility should not prepare as if the audit were a broad review of all manufacturing activities. The audit will focus on the process family, materials, equipment, controls, tests, and records connected to the approval scope.
This sounds straightforward, but scope mistakes create avoidable problems. A supplier may include processes it does not routinely perform, exclude a subcontracted activity that affects final conformity, or rely on procedures written for a different alloy family or customer requirement. The result is often a mismatch between the capability claimed in the audit package and the evidence available in production.
Before preparation begins, map each process flow from receiving through final release. Identify:
- Which aerospace parts, material forms, and alloy families are included;
- Which steps are performed internally and which are outsourced;
- Which customer specifications, drawings, purchase-order requirements, and internal procedures govern the work;
- Which equipment, fixtures, measuring devices, chemicals, test methods, and software support the process;
- Which records demonstrate that every required step occurred as specified.
For advanced metallic materials, this mapping matters because process controls are not interchangeable. Titanium alloys, nickel-based superalloys, high-strength steels, aluminum alloys, and precision castings can have very different handling limits, thermal cycles, atmosphere requirements, contamination risks, and inspection criteria. A procedure that appears comprehensive may still fail to address the material-specific condition that affects the product.
What a Nadcap audit is really testing
An audit generally tests the link between requirements and execution. Auditors do not assess procedures merely because they exist. They look for objective evidence that the approved procedure is current, understood, used at the point of work, supported by capable equipment, and reflected in complete records.
That makes Nadcap certification less about presenting a polished document set and more about proving process discipline. A strong system answers several questions without forcing the auditor to infer the answer:
The most useful preparation method is to trace actual production jobs through these questions. Select representative work orders, including difficult material conditions, rework, interrupted runs, or jobs involving multiple approvals. If a record cannot be followed from incoming material to final release, the system is vulnerable even when individual documents look acceptable.
Heat treatment preparation: where process control becomes material performance
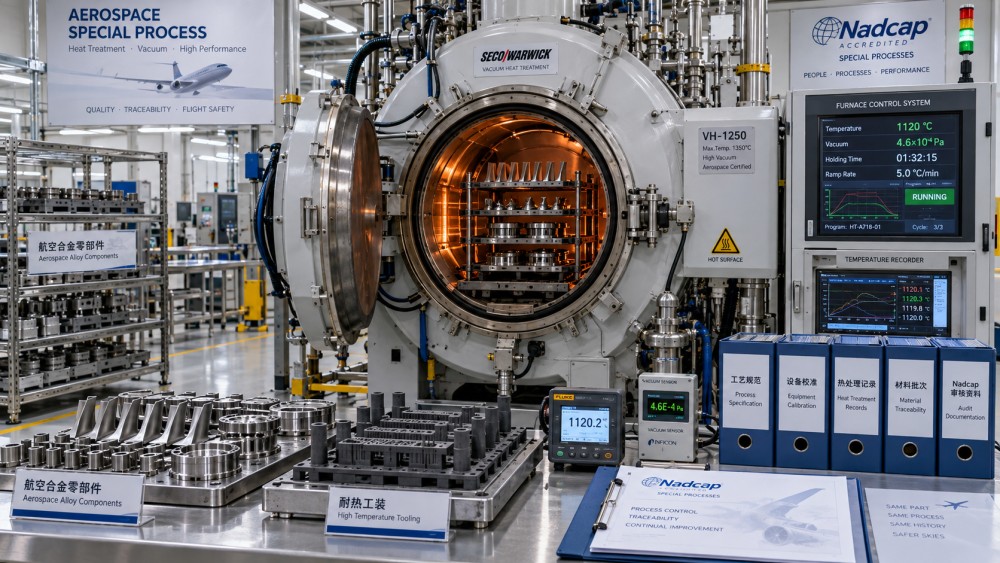
Heat treatment is a common Nadcap focus because the required properties of aerospace metals often depend on tightly controlled thermal history. The concern is not limited to achieving a target temperature. It includes load configuration, temperature uniformity, sensor control, time at temperature, quench or cooling conditions, atmosphere, handling before and after treatment, and the integrity of the recorded data.
For example, an incomplete batch record may prevent a supplier from proving that an age-hardening cycle for a high-strength aluminum alloy was performed correctly. A poorly defined loading instruction may make the response inconsistent between operators. In nickel superalloy processing, a furnace cycle that is nominally correct may still be inadequate if the applicable material condition, part geometry, or atmosphere control was not addressed. These are process-control problems with metallurgical consequences.
Preparation should therefore connect technical instructions to the actual equipment and production environment. Check whether the instructions specify what operators must do when a deviation occurs: a power interruption, alarm event, incorrect load arrangement, out-of-tolerance temperature reading, delayed quench, missing recorder trace, or uncertain part identification. An instruction that only describes normal operation leaves the organization exposed during the conditions that most need control.
Do not confuse calibration with full process readiness
A calibration certificate is necessary, but it does not prove that a process is capable. The broader question is whether the measurement system performs reliably in the operating environment and whether its use is controlled. For thermal processes, that includes the relationship among furnace controls, recording instruments, thermocouples, load sensors, alarm functions, data review, and required checks of furnace performance.
The same principle applies outside heat treatment. In chemical processing, concentration checks and bath maintenance must connect to job requirements and traceability. In non-destructive testing, approved technique, equipment performance, inspection conditions, personnel authorization, and interpretation records must align. In welding, the joint configuration, procedure qualification, filler control, welder authorization, and inspection results must be traceable to the work performed.
Common nonconformities are usually system gaps, not isolated paperwork errors
Documentation gaps are visible during an audit, but their root cause often sits deeper in the operating system. The following issues recur because they arise when procedures are written apart from daily production.
- Outdated or conflicting instructions: The quality system contains a current master procedure, while the work area retains an older copy, locally modified instruction, or obsolete specification reference.
- Records completed after the fact: Data are recreated from memory or transferred manually without clear control. This weakens the credibility of the entire job record.
- Incomplete traceability: Material, lot, part, load, test coupon, process run, and final release cannot be connected without assumptions.
- Training that proves attendance but not capability: A training matrix may show completion, yet there is no evidence that an individual can perform a critical task independently or recognize an unacceptable condition.
- Corrective actions that fix the symptom only: A missing signature is added, but the process that allowed an unsigned record to move forward remains unchanged.
- Weak control of subcontracted work: The purchase order does not pass down the required process instructions, revision level, acceptance criteria, or documentation expectations.
One frequent error is treating every finding as a documentation issue. If a record is missing because production releases work before review, the corrective action needs to address release control, responsibility, workflow design, and verification. Adding a reminder to the form may close a local gap without controlling the risk.
A practical preparation sequence
Preparation is more effective when it is organized around evidence and execution rather than a last-minute document review. The sequence below works well for special-process operations because it exposes gaps early enough to correct them through normal work.
- Build a requirement-to-evidence matrix. List the applicable audit criteria and identify the specific procedure, record, equipment file, training file, or production observation that demonstrates compliance. Avoid assigning vague evidence such as “quality manual.”
- Review controlled documents at the work location. Confirm that operators can access the right revision and that instructions are usable under production conditions. A technically correct procedure is ineffective if its critical limits are difficult to find or its terminology differs from the job traveler.
- Audit representative jobs backward and forward. Start with a completed part and trace backward to material receipt; then start with incoming material and trace forward to release. This exposes traceability breaks that a document-only review can miss.
- Verify equipment status on the shop floor. Compare equipment identification, maintenance status, calibration labels, alarms, software version control where relevant, and actual operating practice with the documented system.
- Test deviation handling. Review real or simulated abnormal conditions. Determine who stops the process, who evaluates the product, how affected material is contained, and how the final disposition is recorded.
- Run a focused internal audit. Use auditors who understand the process well enough to challenge the evidence trail. The goal is not to reproduce a ceremonial external audit; it is to identify where normal work diverges from controlled work.
Prepare people to explain the process, not recite the manual
Interview readiness matters because an audit includes the people performing and supervising the work. Personnel should be able to explain what they do, which instruction they use, how they know the equipment is acceptable, what data they record, and what they do when something falls outside the stated limit.
Coaching should not turn into scripted answers. Scripted responses are fragile because follow-up questions quickly reveal whether the process is understood. A better approach is to walk through actual work with the relevant operator, inspector, planner, or supervisor. Ask them to show the applicable instruction, identify the current job requirement, explain the hold points, and locate the evidence generated during the process.
Clear responsibility boundaries are equally important. When a process deviation occurs, employees must know whether they can adjust a setting, stop the job, quarantine the product, notify supervision, or initiate a nonconformance record. Ambiguity can cause a small equipment or handling event to become an uncontrolled product risk.
Corrective action should prove containment, cause, and effectiveness
A Nadcap finding should be handled as a process failure that needs a durable correction. A strong response distinguishes between immediate containment and permanent corrective action. Containment protects potentially affected work now. Root-cause analysis explains why the system allowed the condition. Corrective action changes the system so the condition is less likely to recur. Effectiveness review verifies that the change works in routine production.
Broad statements such as “retrained employees” or “updated the procedure” are rarely persuasive on their own. The response should make the mechanism clear. If an outdated specification was used, for example, the corrective action may need to address document distribution, revision alerts, removal of uncontrolled copies, planning review, and verification before job release. The evidence should show that each relevant control was implemented.
Do not close a finding based only on a revised document. Use subsequent jobs, completed checks, audit samples, or system records to demonstrate that the revised control has entered normal practice.
When certification readiness also improves supplier confidence
The discipline developed for Nadcap certification has value beyond the audit itself. Buyers of aerospace alloys, forgings, castings, extrusions, and finished components need confidence that special-process results are reproducible and traceable. A supplier that can clearly show process capability, material control, technical documentation, and disciplined response to deviations is easier to evaluate than one that relies on general statements about quality.
For organizations working with complex metallic materials, technical intelligence can also support preparation. Resources such as Global Advanced Alloys & Metallurgy Systems (AAMS) can help connect Nadcap heat treatment and process-control questions with the metallurgical behavior of titanium alloys, superalloys, specialty steels, aluminum products, and precision castings. That context is useful when converting a broad quality requirement into a control that protects a real material property.
The final readiness check is simple: select any recent production job and ask whether an independent reviewer can understand what was required, what was done, who performed it, what equipment was used, how deviations were handled, and why the released result is acceptable. If the answer depends on verbal explanation, undocumented knowledge, or assumptions between disconnected records, the process needs more work before the audit.
Related News
- Nadcap Certification: Audit Requirements and Preparation for Aerospace SuppliersSep 20, 2026Nadcap certification guide for aerospace suppliers: understand audit requirements, special-process controls, common gaps, and practical preparation steps.
- How to Qualify U.S. Defense-Grade Materials for Traceability and ComplianceSep 19, 2026Defense grade materials USA: learn how to qualify suppliers, maintain end-to-end traceability, verify test records, and strengthen defense compliance with audit-ready controls.
- Nickel-Cerium Alloy Selection Criteria for High-Temperature Aerospace ComponentsSep 11, 2026Nickel cerium alloys boost thermal stability & oxidation resistance in jet engine hot sections—discover key selection criteria for aerospace reliability.
- Alloy Characterization Methods: Choosing Tests for Aerospace Material QualificationSep 11, 2026Alloy characterization methods for aerospace qualification: select chemistry, microstructure, mechanical, NDT, and environmental tests that prove service-ready performance.