When Commodity Management Metals Programs Reduce Supply Disruption Risk
Commodity management metals programs are becoming essential for manufacturers that cannot treat material availability as a routine purchasing issue. Volatile prices are only one part of the problem. Export restrictions, concentrated mining and refining capacity, long qualification cycles, inconsistent melt quality, shipping interruptions, and sudden demand shifts can all stop production long before a procurement team has time to negotiate a better price.
The risk is especially visible in advanced manufacturing. A turbine component may depend on a nickel-based superalloy with tightly controlled chemistry and heat-treatment history. An EV drive system may rely on NdFeB magnets whose magnetic properties depend on both rare-earth availability and processing expertise. A battery supplier may need copper foil with application-specific thickness, surface condition, and consistency. In these settings, “metal” is not a fully interchangeable commodity. Its physical form, traceability, processing route, and qualification status matter as much as market price.
A well-designed commodity management metals program reduces disruption risk when it connects commercial decisions to metallurgical reality. It does not promise that shortages will disappear. It gives decision-makers earlier warning, more credible alternatives, and clearer rules for deciding when to protect supply, redesign a part, adjust inventory, or accept a calculated exposure.
The point at which normal buying stops being enough
Traditional purchasing processes work reasonably well for materials with broad supplier bases, standard specifications, and short replacement cycles. They become fragile when a material is technically critical but commercially concentrated. This is common with titanium mill products, aerospace-grade aluminum, cobalt- and nickel-containing alloy inputs, tungsten materials, specialty steel grades, rare earth permanent magnets, beryllium copper, and high-performance copper foils.
The trigger is not necessarily a dramatic market event. A program should be considered when one of several conditions appears: a single qualified source supports a production-critical part; lead times are longer than the company’s planning horizon; a change in feedstock origin can affect certification or product performance; material demand is rising faster than internal visibility; or engineering cannot easily approve a substitute. In such cases, buying at the lowest current price can create a much larger downstream cost if a line stops or an approved material route is lost.
The most exposed organizations often discover the issue indirectly. They may have a purchase order that is technically confirmed but lacks a reliable melt schedule, a magnet supplier unable to clarify rare-earth sourcing, or an extrusion producer dependent on billet grades that are not available in the expected delivery window. The immediate problem looks operational, but its causes are usually spread across engineering, quality, logistics, finance, and supplier management.
Commodity management is not simply hedging
Price hedging can be useful for selected exposure, particularly where market benchmarks exist and the purchased material closely follows them. Yet financial hedges do not secure physical metal, qualify an alternate producer, confirm a heat-treatment route, or solve a compliance requirement. A commodity management metals program therefore needs a wider scope: market exposure, physical availability, technical interchangeability, supplier capability, and the consequences of failure.
Consider copper. A company may hedge general copper price exposure while remaining vulnerable to a shortage of a particular rolled foil or high-conductivity alloy product. The metal value may be protected, but the converting capacity, foil treatment, width tolerance, and delivery allocation may not be. The same distinction applies to nickel or titanium: an exchange or index can indicate price direction, but it cannot represent the full availability of qualified vacuum-melted stock, forged bar, plate, powder, or precision casting feedstock.
This is why program governance should not sit exclusively in either treasury or procurement. Finance should understand the exposure. Procurement should manage contracts and supplier relationships. Engineering and quality must define what can truly be replaced, under which test requirements, and with what documentation. Operations need to show the real production consequence of a shortage rather than just annual spend.
Map criticality by material route, not by spend alone
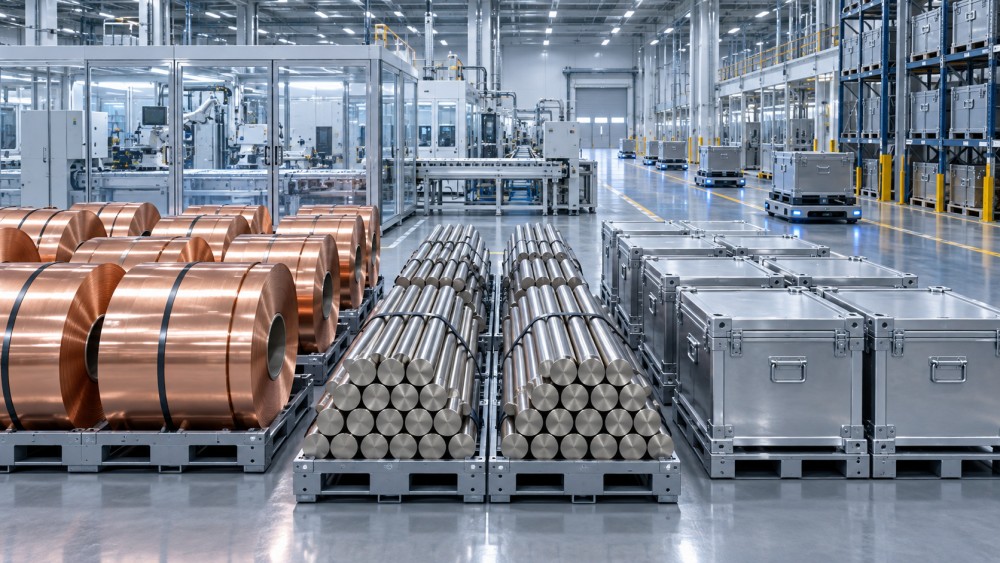
A common mistake is to prioritize commodities solely by annual purchasing value. That approach can overlook a relatively low-spend item that has no qualified substitute and can halt shipment of a much higher-value assembly. A better assessment separates economic exposure from operational criticality.
For every critical metal input, teams should identify the exact material condition required: alloy designation, relevant chemistry limits, product form, dimensions, required mechanical properties, heat treatment, surface condition, traceability level, and applicable customer or industry specifications. “Titanium” is not a usable risk category if the actual requirement is a specific aerospace-grade bar with controlled ultrasonic inspection and a defined documentation package. “Rare earths” is similarly too broad where a motor design depends on a magnet grade with particular temperature resistance and grain-boundary diffusion characteristics.
The next question is where the bottleneck actually lies. It may be mine output, chemical conversion, refining, alloying, melting, rolling, sintering, machining, coating, or final inspection. In powder metallurgy and cemented carbide supply chains, for example, availability of tungsten feedstock does not automatically mean that the required powder characteristics or carbide tool blanks can be supplied. Each conversion step can create its own concentration and lead-time risk.
Where diversification works—and where it can backfire
Supplier diversification is often the first recommendation, but it should not mean adding names to an approved vendor list without checking process equivalence. A second supplier can reduce risk only if it can provide material that is acceptable in the actual application and can sustain delivery under pressure. For advanced alloys, this may involve reviewing melting practice, forging or rolling capability, heat-treatment control, non-destructive testing, and lot traceability. For magnets, powder, castings, or foil, the variables are different but no less material.
Diversification also has a cost. Splitting small volumes among too many suppliers can weaken commercial commitment, complicate quality control, and reduce visibility into actual capacity. The more useful model is usually tiered: a primary source for normal production, a qualified secondary source for defined volumes or emergency allocation, and an intelligence process that monitors upstream dependencies. Certain materials may require regional diversity; others need diversity across processing technologies or recycling routes.
Technical substitutes should be treated with the same discipline. Replacing a high-temperature nickel alloy, changing an aluminum casting alloy, or altering a magnetic material can affect fatigue behavior, corrosion resistance, machinability, thermal performance, or end-product certification. A substitution may be commercially sensible, but only after engineering establishes the performance window and quality determines the required validation. The right question is not “Can we use another metal?” but “What properties are non-negotiable in this component, and what evidence is needed to change the route?”
Inventory becomes useful when it is tied to recovery time
Buffer inventory is frequently criticized as expensive, and it can be when applied without logic. Yet lean inventory rules designed for stable supply may be unsuitable for materials with lengthy qualification and replenishment cycles. The objective is not to stockpile everything. It is to hold protection where the time needed to recover supply exceeds the time the operation can tolerate without the material.
This calculation should include more than supplier lead time. Recovery time can include release of raw material, melting or conversion, testing, transport, incoming inspection, and internal scheduling. It should also account for whether the company can use a different lot, a different source, or recycled content without additional approval. In some applications, strategic inventory may be more practical as semi-finished stock than as raw metal, especially when a particular extrusion profile, powder grade, foil width, or casting feedstock has limited availability.
Inventory quality matters too. Materials with shelf-life considerations, corrosion sensitivity, handling controls, or traceability requirements cannot simply be stored and forgotten. Lot segregation, certificate retention, stock rotation, and clear ownership of release decisions are part of resilience. A warehouse full of material that cannot be matched to the required documentation is not a reliable buffer.
Traceability turns market intelligence into an operating decision
Market news has limited value if it cannot be linked to the materials and components that a business actually uses. The strongest programs connect external signals to internal bills of materials, supplier locations, material specifications, and production commitments. That makes it possible to ask practical questions: Which customer programs depend on this alloy family? Which parts use a source exposed to a particular region or converter? Which open orders are affected if capacity tightens? Which lots have complete documentation for a regulated or safety-critical application?
This linkage is particularly relevant where export controls, origin questions, or customer flow-down requirements may affect a supply route. Requirements vary by market and application, so companies should avoid assumptions based on general commodity headlines. Legal, trade, and compliance teams need to review the relevant obligations, while technical teams confirm whether alternative sources meet the part-level requirements.
AAMS is useful in this context because it brings material science, supplier visibility, commodity risk, and industrial application into the same discussion. For a buyer assessing copper concentrate risk, rare-earth export developments, or alloy capacity, the essential follow-up is always technical: what does this signal mean for the grade, process route, performance requirement, and documentation needed by the factory? Intelligence becomes actionable only when those links are visible.
Build the program around decisions, not reports
Many risk initiatives fail because they produce dashboards without assigning decisions. A credible program should define thresholds and actions in advance. If a qualified supplier’s lead time moves beyond an agreed boundary, who authorizes additional coverage? If a supply region becomes exposed, when does alternate qualification begin? If a price move is driven by a short-term market event, what level of exposure warrants contract review rather than panic buying?
The answers will differ across business models. Aerospace and defense supply chains may place greater weight on qualification continuity and documented process control. Automotive lightweighting programs may focus on aluminum conversion capacity, tooling schedules, and the effect of alloy changes on casting performance. Tooling manufacturers may need closer visibility into tungsten, cobalt, powder processing, and carbide-grade consistency. Battery and electronics supply chains may concentrate on copper foil specification, coating compatibility, and volume allocation. One corporate rule rarely fits all of them.
A practical starting point is to select a limited set of materials that combine high operational criticality with constrained substitution. Map their routes, validate supplier dependencies, identify documentation gaps, and agree on the actions that follow a warning signal. Only then should the organization expand the model. This approach is less dramatic than reacting to every commodity headline, but it is more likely to protect production when disruption reaches the factory gate.
Commodity management metals programs reduce supply disruption risk when they respect a basic industrial fact: the metal market and the manufactured component are connected, but they are not the same thing. The businesses best prepared for interruption know which materials are truly irreplaceable, how long recovery would take, and what technical evidence is required before changing course. Those are the details worth confirming before the next shortage makes them urgent.
- powder metallurgy
- NdFeB magnets
- beryllium copper
- precision casting
- copper concentrate risk
- specialty steel
- automotive lightweighting
- specialty steel grades
- rare earth permanent magnets
- advanced alloys
- heat treatment
- aluminum casting
- metallurgy
- permanent magnets
- copper foil
- powder processing
- corrosion resistance
- export controls
Related News
- Aerospace Superalloy Price Trends: How Nickel, Energy, and Supply Risk Shape CostsSep 22, 2026Aerospace superalloys price trend: see how nickel, energy costs, qualified capacity, and supply risk shape alloy pricing, lead times, and smarter sourcing decisions.
- When commodity management metals programs reduce supply disruption riskSep 22, 2026Commodity management metals programs help manufacturers reduce supply disruption risk through smarter sourcing, traceability, qualified alternatives, and recovery-focused inventory strategies.
- What nonferrous metals price trends mean for annual sourcing budgetsSep 21, 2026Nonferrous metals price trends can reshape annual sourcing budgets. Learn to model exposure, manage contracts, and protect cash, margins, and supply continuity.
- Alloy Sourcing in the USA: How Buyers Can Qualify Suppliers and Reduce Supply RiskSep 16, 2026Alloy sourcing USA guide: qualify suppliers, verify traceability, control costs, and reduce supply risk with practical buyer strategies.